
CASE STUDY · KERRY · EUROPE
Gas-to-Gas Heat Recovery with CIP Cleaning for Kerry
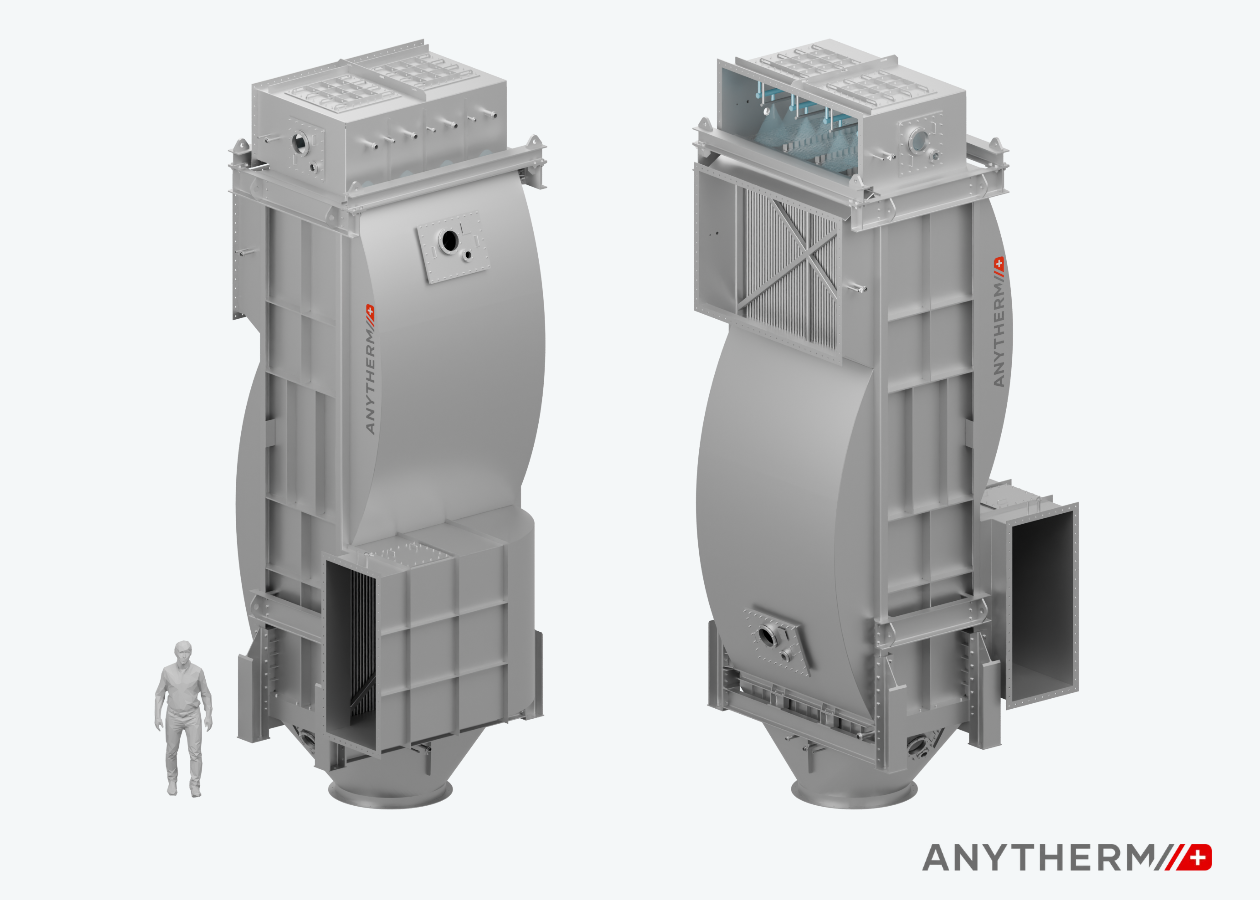
Anytherm has delivered a new gas-to-gas heat recuperator for a spray drying application at a Kerry food ingredients production site in Europe. The repeat order builds on a previously supplied unit and reflects the customer’s continued trust in Anytherm’s engineering and project execution.
The system recovers heat from exhaust air and transfers it directly to the incoming process air. With a heat recovery capacity of approximately 800 kW, it helps reduce the process’s external heat demand and operating costs.
Project highlights
- Approx. 800 kW heat recovery capacity
- Around 1,500 stainless steel tubes for heat transfer
- Over 10,000 kg of equipment, with fully stainless steel construction
- Integrated CIP system for cleaning the heat transfer surfaces during operation
- FEM analyses for explosion safety, thermal expansion and lifting conditions
- CFD-supported duct design for optimised flow distribution
- Custom lifting concept for safe handling and installation
Recovering exhaust heat for spray drying
The recuperator uses the exhaust air’s thermal energy to preheat incoming air streams. At continuous operation at the stated recovery capacity, the theoretical annual heat recovery is approximately 7,000 MWh. Actual recovery depends on operating hours, temperatures and process conditions.
For illustration, assuming an avoided emissions factor of 0.2 tonnes of CO₂ per MWh of recovered heat, this would correspond to approximately 1,400 tonnes of CO₂ per year. These figures describe a calculated potential, rather than measured annual savings. Site-specific emissions depend on the heat source displaced.

Engineering beyond the heat exchanger
The project included engineering support for the inlet and outlet ducting to establish suitable flow conditions and integrate the recuperator into the overall process. Structural analyses addressed thermal expansion, explosion safety and lifting conditions, complemented by a custom lifting concept.
CIP cleaning during operation
The integrated cleaning-in-place (CIP) system cleans the heat transfer surfaces during the process. The cleaning arrangement is integrated into the recuperator design and tailored to the application.
The second view shows the tube rows and upper tube sheet. CIP piping and spray patterns are highlighted in blue; the spray is shown schematically.
Direct gas-to-gas or a water loop?
DIRECT HEAT TRANSFER
Gas-to-gas heat recovery
Heat passes through the metal tube walls from exhaust air to process air within one unit.
- One recuperator: no intermediate water circuit.
- Plant layout: both air streams are routed to the unit.
- Design focus: cleaning access, pressure losses and the required separation of the air streams.
CONNECTED HEAT RECOVERY
Heat recovery with a water loop
Separate exhaust air recuperators and air preheaters are connected by a water circuit.
- Flexible connections: heat sources and users can be in different locations.
- System integration: several heat sources and users can be connected.
- Design focus: pumps, piping, controls and additional temperature differences across the heat exchangers.
The best choice depends on the plant layout, temperature levels, operating profile and cleaning requirements. Anytherm combines equipment engineering with heat recovery and pinch analysis to identify suitable heat recovery systems for each process.
From fabrication to dispatch
A look behind the scenes at Anytherm BH in Bosnia and Herzegovina, where the Kerry recuperator was manufactured: from the tube sheet and heat exchanger assembly to protective packaging and dispatch.
During manufacturing
From assembly to dispatch
A partnership that goes back to our early years
The recuperator supplied in 2019 to a company now part of the Kerry Group was one of Anytherm’s first large single units, with a unit weight of 30 tonnes. The photograph shows brothers and founders Dominic and Nicolas Ettlin beside the original unit before delivery — a reminder of the company’s early years.
From the start, our aim was to build relationships that last beyond a single project. It is therefore particularly rewarding to see this collaboration continue with a repeat order for Kerry. Thank you for the trust, teamwork and collaboration over the years.
Let’s discuss heat recovery for your process
Tell us about your process, available waste heat and cleaning requirements. Our sales engineers and energy consultants will help you assess a suitable approach — from the first heat recovery assessment to the equipment concept.
A short project outline is enough to start. The guided enquiry helps you collect the key points; you can also contact our team directly.