
Heat transfer | Heat recovery | Energy efficiency
Industrial Heat Recuperators
Turn exhaust air and flue gas into useful process heat. Custom recuperators, cleanable heat exchanger elements and complete water-loop systems – backed by heat recovery and pinch analysis expertise.

The right heat recovery concept
Direct gas-to-gas or a water loop?
Direct gas-to-gas recovery
The hot and cold gas streams pass through one unit. Heat crosses the separating metal surfaces without an intermediate water circuit. Both streams must be routed to the recuperator.
Indirect recovery via water
Separate exhaust-air recuperators and preheaters are connected by a water circuit. This can suit heat sources and users in different locations or systems with several heat sources and consumers.
Designed around your process
- Custom exhaust air and flue gas heat recovery units.
- Finned-tube, bare-tube and pillow-plate heat exchangers.
- Extractable elements and cleaning-in-place options.
- Condensation heat recovery where suitable for the process.
- Preheaters, pumping stations, piping and instrumentation within the agreed scope.
Dust loading, deposits, chemical composition and condensation influence the choice of materials and heat transfer geometry. Thermal performance, pressure loss, stream separation and cleanability are considered together.
| Parameter | Design / scope |
|---|---|
| Air mass flow | Up to 200,000 kg/h per unit |
| Housing | AISI 304 or AISI 316 stainless steel with mineral wool insulation |
| Finned tubes | AISI 304 or AISI 316 stainless steel |
| Fins | Aluminium or stainless steel; stainless steel for suitable CIP duties |
| Operating temperatures | Selected for the application, media and additional equipment |
Indicative design information. Limits depend on the duty, materials and configuration and do not necessarily apply simultaneously. Final performance is confirmed for the agreed operating conditions.
Why Anytherm
Equipment engineering meets energy expertise.
Heat recovery and pinch expertise
We connect equipment selection with useful heat demand. Our analysis helps identify suitable temperature levels, operating profiles and integration opportunities.
Cleaning designed into the equipment
Surface geometry, maintenance access, drainage and CIP are considered from the start, according to the actual media.
Engineering through to delivery
We coordinate thermal and mechanical design, installation interfaces and the agreed equipment scope. Your team has a direct engineering contact.
Equipment in practice
Different processes. Different recuperator designs.
Exhaust air to water
A cleanable exhaust-air recuperator transfers recovered heat to a water circuit. The circuit connects the exhaust side with a preheater or other suitable heat user.
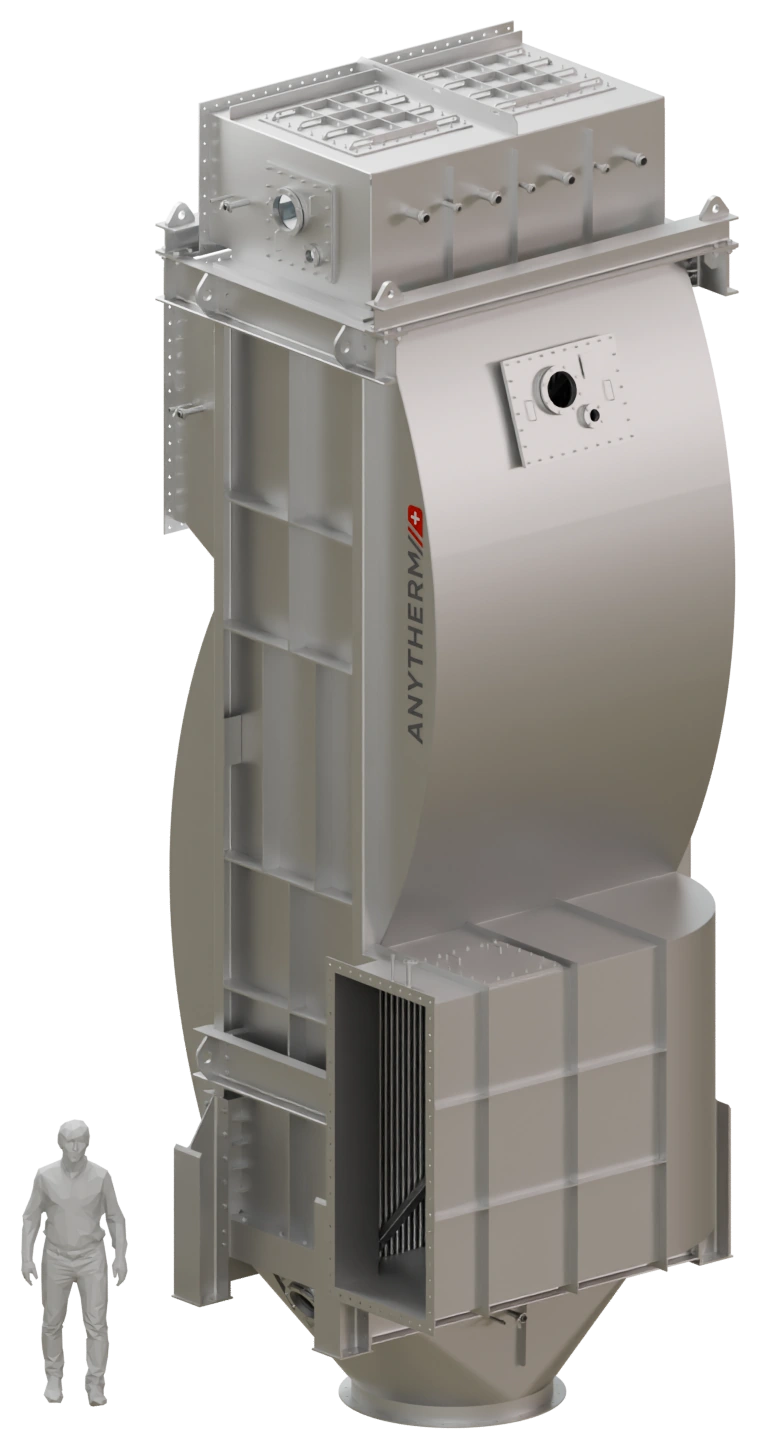
Exhaust air to process air
The Kerry recuperator recovers approximately 800 kW directly between gas streams. Its stainless steel construction includes around 1,500 tubes and integrated CIP cleaning.
Nestlé
Delivered equipment. Heat integration expertise.
By July 2024, Anytherm had delivered three large exhaust air recuperators with heat recovery capacities of approximately 1.3–2 MW per unit. The equipment includes condensation heat recovery and integrated CIP. The Nestlé case study also describes a separate site-wide pinch study. Its identified savings potential is distinct from the capacity of the delivered equipment.
More reference projects
Exhaust-air and flue-gas recuperators around the world.
Selected project references show different unit geometries, condensation heat recovery and integrated air intake systems. Each design is adapted to its process and installation.
Netherlands · 2019
30,000 kg gas-to-gas recuperator with integrated CIP. Delivered to a company now part of the Kerry Group.
England
Flue-gas recuperator
Germany
Flue-gas recuperator unit
Norway
Flue-gas recuperator
Thailand
Flue-gas recuperator
Germany · Chemical industry
Exhaust-air recuperator unit
Germany · Pharmaceutical industry
Exhaust-air recuperator
Netherlands
Exhaust-air recuperator with condensation heat recovery
France
Exhaust-air recuperator with condensation heat recovery
Denmark
Exhaust-air recuperator
Germany
Air intake unit with integrated gas-to-gas heat recovery and CIP
Before equipment selection
Find the best use for recovered heat.
A heat recovery or pinch analysis matches available sources with demand at suitable temperature levels. Operating hours, useful recovered energy, energy prices and installation costs determine the economics. We assess payback for the actual project rather than treating exchanger capacity as annual savings.
Practical questions
Can contaminated gas streams be used?
Yes, where materials, spacing and cleaning can be matched to the media. Please share the gas composition, dust or deposit characteristics and cleaning requirements so we can assess the duty.
Can condensation heat also be recovered?
For suitable processes, cooling below the condensation temperature can recover additional heat. Materials, drainage, corrosion and cleaning requirements must be considered in the design.
Which information helps with an enquiry?
Useful starting points are gas or air mass flow, inlet and target temperatures, operating hours, contamination, permissible pressure losses and the available installation space. Preliminary values are welcome.
Let’s talk about your process
Discuss your project with our engineering team.
Share your process, operating conditions and what you want to improve. A complete specification is not needed to start a conversation.
[email protected]
+41 78 722 2200
Your heat recovery specialist: Tobias Helbling, Head of Industrial Energy and Heat Recovery.